Get more content that can help you
Content
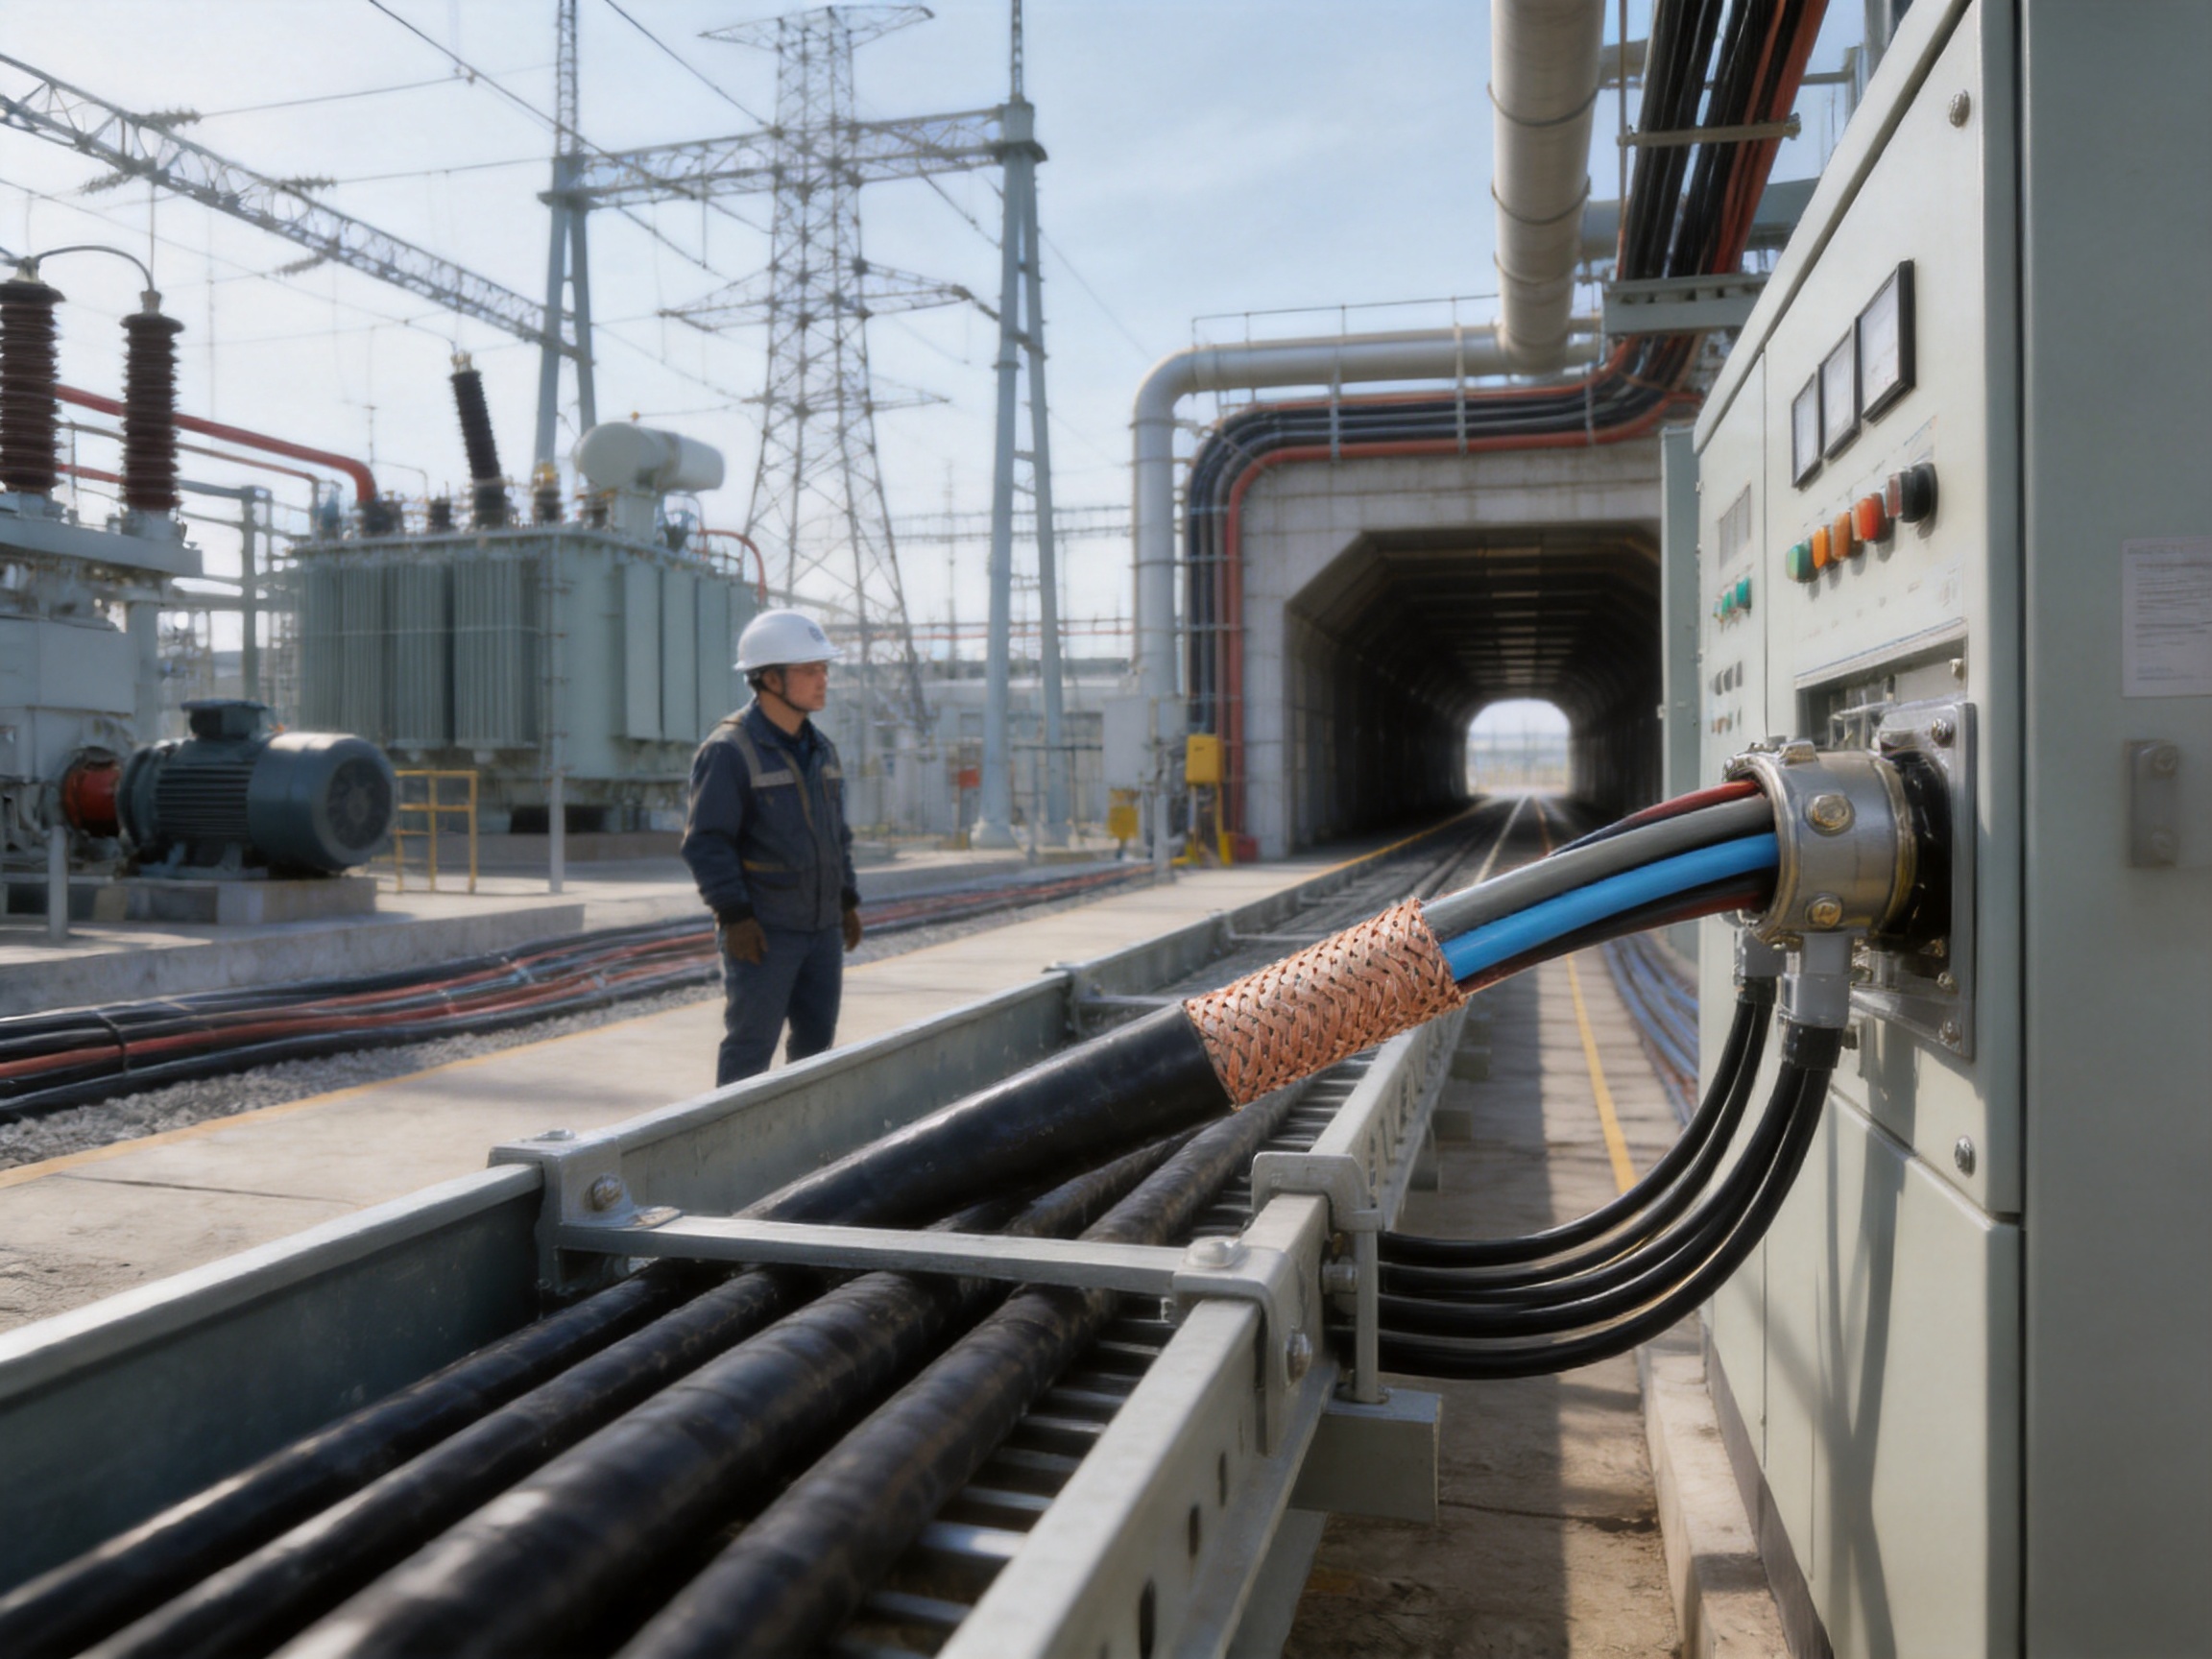
Modern industrial systems depend on control cables that can transmit signals reliably while withstanding heat, electromagnetic interference, moisture, vibration, pressure, and accidental mechanical damage. In a simple indoor installation, a standard PVC control cable may be sufficient. However, demanding industrial environments require a more comprehensive design. Power plants, substations, metallurgical facilities, cable tunnels, production lines, and direct-burial systems often expose cables to several hazards at the same time.
KYJVP22 is designed for these challenging conditions. It combines cross-linked polyethylene insulation, copper braid shielding, double-layer galvanized steel tape armor, and PVC inner and outer sheaths. This combination gives the cable three principal functions: stable operation at elevated temperatures, electromagnetic interference suppression, and mechanical protection against compression and impact.
With a rated voltage of 450/750V, a long-term allowable conductor temperature of 90°C, and configurations ranging from two to thirty-seven cores, KYJVP22 can be adapted to many control, monitoring, instrumentation, and industrial automation applications. Its conductor cross-section range of 1.5 mm² to 10.0 mm² supports both compact control circuits and applications requiring greater current-carrying capacity or stronger mechanical construction.
The cable is manufactured by Anhui Zhishang Cable Technology Co., Ltd., an industrial cable producer integrating research and development, production, testing, sales, and customized cable services. The company operates a modern production base of approximately 5,000 square meters, uses ten automated production lines, and reports monthly production capacity of up to ten million meters. Its manufacturing system supports standard cable production as well as OEM and ODM development based on technical drawings, samples, and project requirements.
This article explains the structure, performance, manufacturing advantages, installation considerations, application range, and selection value of KYJVP22. It also compares the product’s integrated design with more basic control cable constructions and answers common technical questions for engineers, contractors, equipment manufacturers, and purchasing teams.
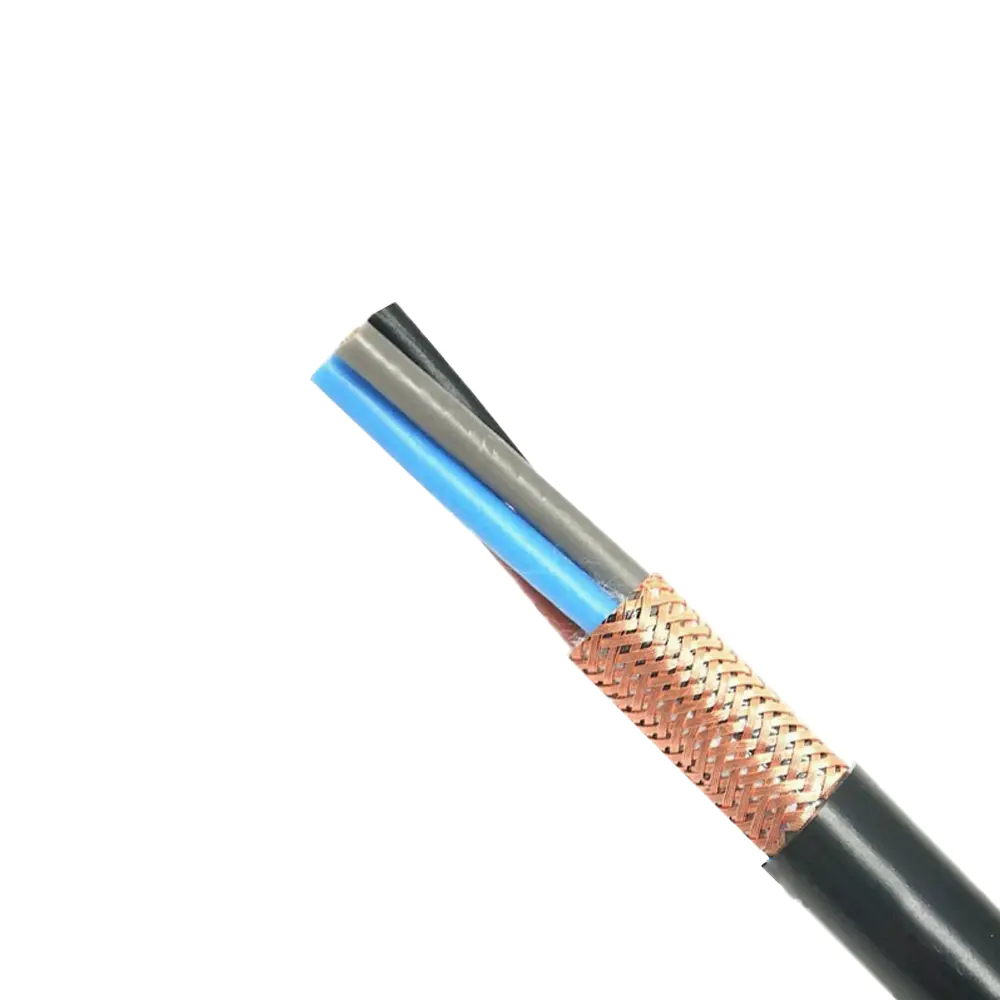
KYJVP22 Combining anti-interference and protection Control Cable
A control cable is responsible for transmitting electrical control, measurement, protection, and monitoring signals. Unlike a cable used only for energy transmission, a control cable may carry information from sensors, switches, actuators, relays, programmable controllers, and protection devices. Signal quality and continuity are therefore essential.
Industrial environments can create several types of stress. High ambient temperatures may accelerate insulation aging. Motors, transformers, variable-frequency drives, switching devices, welding equipment, and high-current conductors may generate electromagnetic fields. Cables installed in cable trays or tunnels may be exposed to vibration, compression, impact, moisture, and corrosive contaminants. Direct-buried cables may also encounter soil pressure, rocks, construction activity, and occasional mechanical disturbance.
A basic unshielded PVC control cable may perform adequately in a clean and electrically quiet indoor area, but it may not provide sufficient protection in a complex industrial environment. Similarly, a shielded cable without armor can reduce interference but remain vulnerable to crushing, impact, and external damage. An armored cable without an effective shield can improve mechanical strength while still allowing electromagnetic noise to affect sensitive signals.
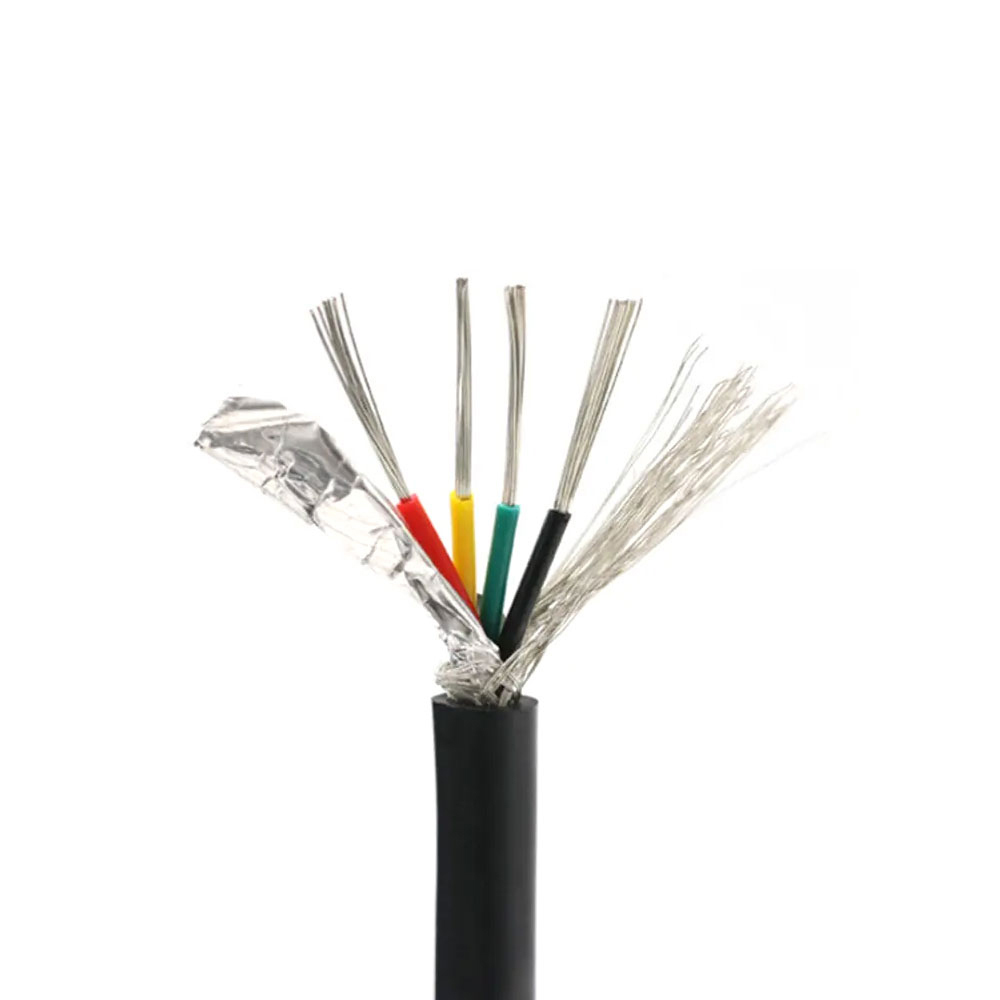
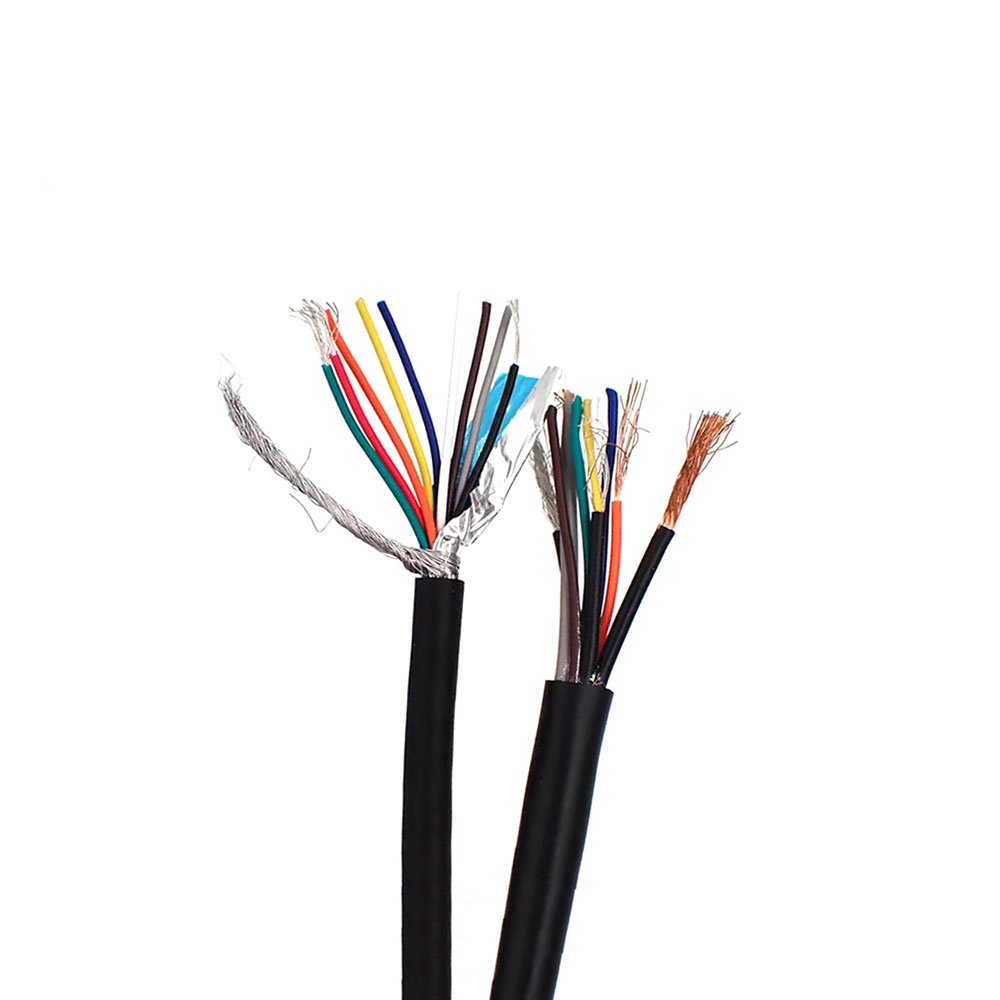
KYJVP22 addresses these issues through a layered structure. The XLPE insulation helps maintain electrical performance at elevated operating temperatures. The copper braid shield provides a conductive barrier that reduces the influence of external electromagnetic interference. The double-layer galvanized steel tape armor adds mechanical protection. The inner and outer PVC sheaths protect the cable assembly against moisture, abrasion, and general environmental exposure.
The value of this design is not simply the presence of multiple materials. The layers work together as a coordinated system. The conductor transmits the signal, the insulation separates individual conductors and controls dielectric behavior, the shield helps manage interference, the armor protects the cable from mechanical stress, and the sheaths preserve the integrity of the entire construction during handling and installation.
KYJVP22 uses solid or stranded annealed copper conductors. Copper provides high electrical conductivity, good termination performance, and reliable compatibility with common industrial connection systems. Annealing improves conductor flexibility and helps reduce the risk of cracking or excessive resistance caused by hard-drawn material.
The product supports conductor cross-sections from 1.5 mm² to 10.0 mm². Solid conductors can provide dimensional stability in fixed wiring applications, while stranded conductors are better suited to installations that require easier routing and termination. The appropriate conductor construction depends on the equipment connection method, installation geometry, current requirements, and customer specifications.
For control circuits, conductor sizing is not determined only by nominal current. Voltage drop, fault conditions, terminal capacity, ambient temperature, grouping, installation length, and future expansion should also be evaluated. The available range gives system designers flexibility when selecting a cable for a compact control cabinet, a long cable run, or a larger industrial control circuit.
The insulation material is cross-linked polyethylene, commonly referred to as XLPE. Compared with ordinary PVC insulation, XLPE generally offers improved thermal capability, stronger resistance to thermal deformation, and stable dielectric performance over a broad range of industrial applications.
KYJVP22 is designed for a long-term allowable operating temperature of 90°C. This rating provides a meaningful advantage over many conventional PVC-insulated control cables that are designed for lower continuous operating temperatures. The higher temperature capability can be useful in power-generation facilities, metallurgical plants, equipment rooms, industrial furnaces, production machinery, and cable routes located near heat sources.
The insulation thickness is specified within a range of 0.8 mm to 1.6 mm, depending on conductor size and cable design. Correct insulation thickness is important because it affects dielectric strength, insulation resistance, cable diameter, flexibility, and overall material balance. The product has a specified test voltage of 3.5 kV AC for one minute and an insulation resistance of at least 1000 MΩ·km at 20°C.
XLPE also contributes to stable electrical behavior by providing low dielectric loss and resistance to partial discharge-related degradation when the cable is correctly designed, manufactured, installed, and operated. These qualities help support long-term reliability in control and monitoring circuits where signal continuity and insulation integrity are important.
The shielding structure consists of a copper braid with a coverage of at least 80 percent. A copper braid creates a conductive protective layer around the insulated core assembly. Its primary purpose is to reduce the influence of external electromagnetic interference and to provide a practical path for induced noise currents when properly bonded and grounded.
Electromagnetic interference may originate from nearby motors, contactors, transformers, power converters, switching systems, welding equipment, and high-current cables. In sensitive control circuits, interference can appear as unstable measurements, false triggering, communication errors, unwanted relay operation, or irregular feedback signals.
The shield is especially useful when the control cable is routed near power cables or installed in an environment containing significant electrical noise. The specified shielding attenuation factor is no greater than 0.8 at 1 MHz under the stated test conditions. Actual field performance depends on cable routing, grounding method, termination quality, equipment design, and the distance from interference sources.
Shielding should not be viewed as an isolated feature. A shield works most effectively when it is terminated according to the system’s grounding philosophy. Poorly connected shield ends, excessive pigtails, unsuitable grounding arrangements, or interruptions in the shield may reduce the benefit. For this reason, installation procedures should define shield continuity, bonding, and termination practices before the cable is installed.
KYJVP22 uses double-layer galvanized steel tape gap-wrapped armor. The armor is designed to improve resistance to external mechanical forces, including compression, impact, handling stress, and accidental contact with surrounding structures.
The double-layer arrangement provides a more substantial protective barrier than a cable without armor. It is particularly useful when cables are installed in industrial areas where tools, equipment, cable supports, maintenance work, or construction activity may create mechanical hazards. The galvanized surface also contributes to corrosion resistance in ordinary industrial environments.
The product has a stated compression strength of at least 2000 N/100 mm and passes the specified impact test associated with IEC 60229 requirements. These characteristics make the cable suitable for fixed installation in cable trays, conduits, tunnels, pipelines, and selected direct-burial applications, subject to project design and local installation regulations.
Armor improves protection, but it does not eliminate the need for correct handling. The cable must not be dragged over sharp edges, bent below its minimum bending radius, crushed by unsuitable clamps, or exposed to conditions beyond its design limits. The stated minimum bending radius is at least fifteen times the cable outer diameter, which should be observed during pulling, routing, and final positioning.
The cable includes an inner PVC sheath with a specified thickness range of 1.0 mm to 1.8 mm and an outer PVC sheath with a specified thickness range of 1.8 mm to 3.0 mm. These sheaths help separate and protect the internal components while providing a practical surface for installation.
The inner sheath supports the assembly of the core group, shield, and armor. The outer sheath protects the completed cable against moisture, abrasion, handling damage, and general environmental exposure. PVC is widely used in industrial cable construction because it offers a practical balance of cost, processability, mechanical performance, and environmental resistance.
The standard product is not described as a flame-retardant or halogen-free cable. However, flame-retardant and halogen-free options can be considered for projects that require additional fire-performance or low-smoke characteristics. Such requirements should be confirmed before ordering because they may affect material selection, cable diameter, production parameters, test requirements, and lead time.
The following table summarizes the principal technical characteristics supplied for KYJVP22. Final cable dimensions, weights, electrical resistance values, and current-carrying capacity should be confirmed against the selected conductor size, number of cores, installation method, ambient conditions, and applicable technical standard.
| Parameter | Specification |
|---|---|
| Product type | KYJVP22 armored shielded control cable |
| Conductor | Solid or stranded annealed copper |
| Conductor cross-section | 1.5 mm² to 10.0 mm² |
| Number of cores | 2 cores to 37 cores |
| Rated voltage | 450/750V |
| Test voltage | 3.5 kV AC for one minute |
| Insulation material | Cross-linked polyethylene |
| Insulation thickness | 0.8 mm to 1.6 mm |
| Shielding | Copper braid, coverage of at least 80 percent |
| Armor | Double-layer galvanized steel tape gap-wrapped armor |
| Inner sheath | PVC, 1.0 mm to 1.8 mm thickness |
| Outer sheath | PVC, 1.8 mm to 3.0 mm thickness |
| Operating temperature | -15°C to +90°C for fixed installation |
| Long-term conductor temperature | 90°C |
| Short-circuit temperature | Maximum 250°C for up to five seconds |
| Minimum bending radius | At least fifteen times the cable outer diameter |
| Insulation resistance | At least 1000 MΩ·km at 20°C |
| Shielding attenuation factor | No greater than 0.8 at 1 MHz |
| Compression strength | At least 2000 N/100 mm |
| Thermal deformation | Passes 150°C, four-hour thermal deformation test |
One of the clearest advantages of KYJVP22 is its XLPE insulation and 90°C long-term operating temperature. Ordinary PVC control cables may be suitable for standard indoor applications, but their continuous temperature capability can be more limited. When installed near hot equipment or in poorly ventilated cable routes, a lower-temperature cable may experience accelerated aging.
The higher thermal rating gives system designers additional operating margin. It can help reduce the risk of insulation deterioration caused by sustained heat, provided that the cable is operated within its stated limits and the overall installation is correctly designed. The 90°C rating does not mean that every surrounding component can withstand 90°C. Terminals, glands, connectors, control devices, and enclosure materials must also be evaluated.
A shielded cable can reduce electromagnetic interference, but shielding alone does not provide substantial resistance to crushing or impact. In a busy industrial facility, a cable can be damaged by falling tools, maintenance activity, sharp support edges, cable tray loading, or accidental contact with vehicles and equipment.
KYJVP22 adds double-layer steel tape armor around the shielded cable assembly. This creates a more comprehensive solution for areas where both electrical noise and mechanical hazards are present. Instead of specifying a separate protective conduit for every exposed route, an armored cable may simplify the installation strategy, although conduit or additional protection may still be required in particularly severe environments.
Unshielded control cables are often adequate in electrically quiet spaces, but they may be vulnerable to induced noise when installed beside power conductors or switching equipment. The copper braid in KYJVP22 provides a conductive shielding layer that helps suppress interference and improve signal stability.
The benefit is especially relevant to analog signals, sensor circuits, relay controls, instrumentation loops, and monitoring systems. A stable shield can help reduce unwanted signal variation and false operation. Nevertheless, cable selection must be combined with appropriate separation from high-power circuits, correct grounding, suitable cabinet layout, and good termination practices.
The combination of XLPE insulation, shielding, armor, and PVC sheathing allows KYJVP22 to serve several fixed-installation environments. These include indoor industrial spaces, cable trays, equipment rooms, pipelines, cable tunnels, substations, power plants, and selected outdoor or direct-burial routes.
Each installation still requires a site-specific assessment. Direct burial may require attention to drainage, soil chemistry, burial depth, external protection, identification, and local regulations. Outdoor installations may require UV exposure evaluation. Cable tunnels may require fire-performance, smoke, and emergency-access considerations. The cable’s layered construction provides a strong foundation, but engineering conditions determine whether additional measures are necessary.
A cable that combines insulation, shielding, armor, and protective sheathing may offer a better overall project value than a lower-cost cable that requires extensive supplementary protection. The initial unit price should not be the only purchasing criterion. Installation labor, conduit, protective covers, replacement risk, downtime, troubleshooting, and maintenance can significantly affect total ownership cost.
KYJVP22 is positioned as a cost-effective solution within the category of high-temperature, shielded, armored control cables. Its integrated structure can reduce the need to combine an ordinary control cable with additional shielding or mechanical protection. The final economic benefit depends on cable length, route complexity, local labor rates, environmental severity, and project specifications.
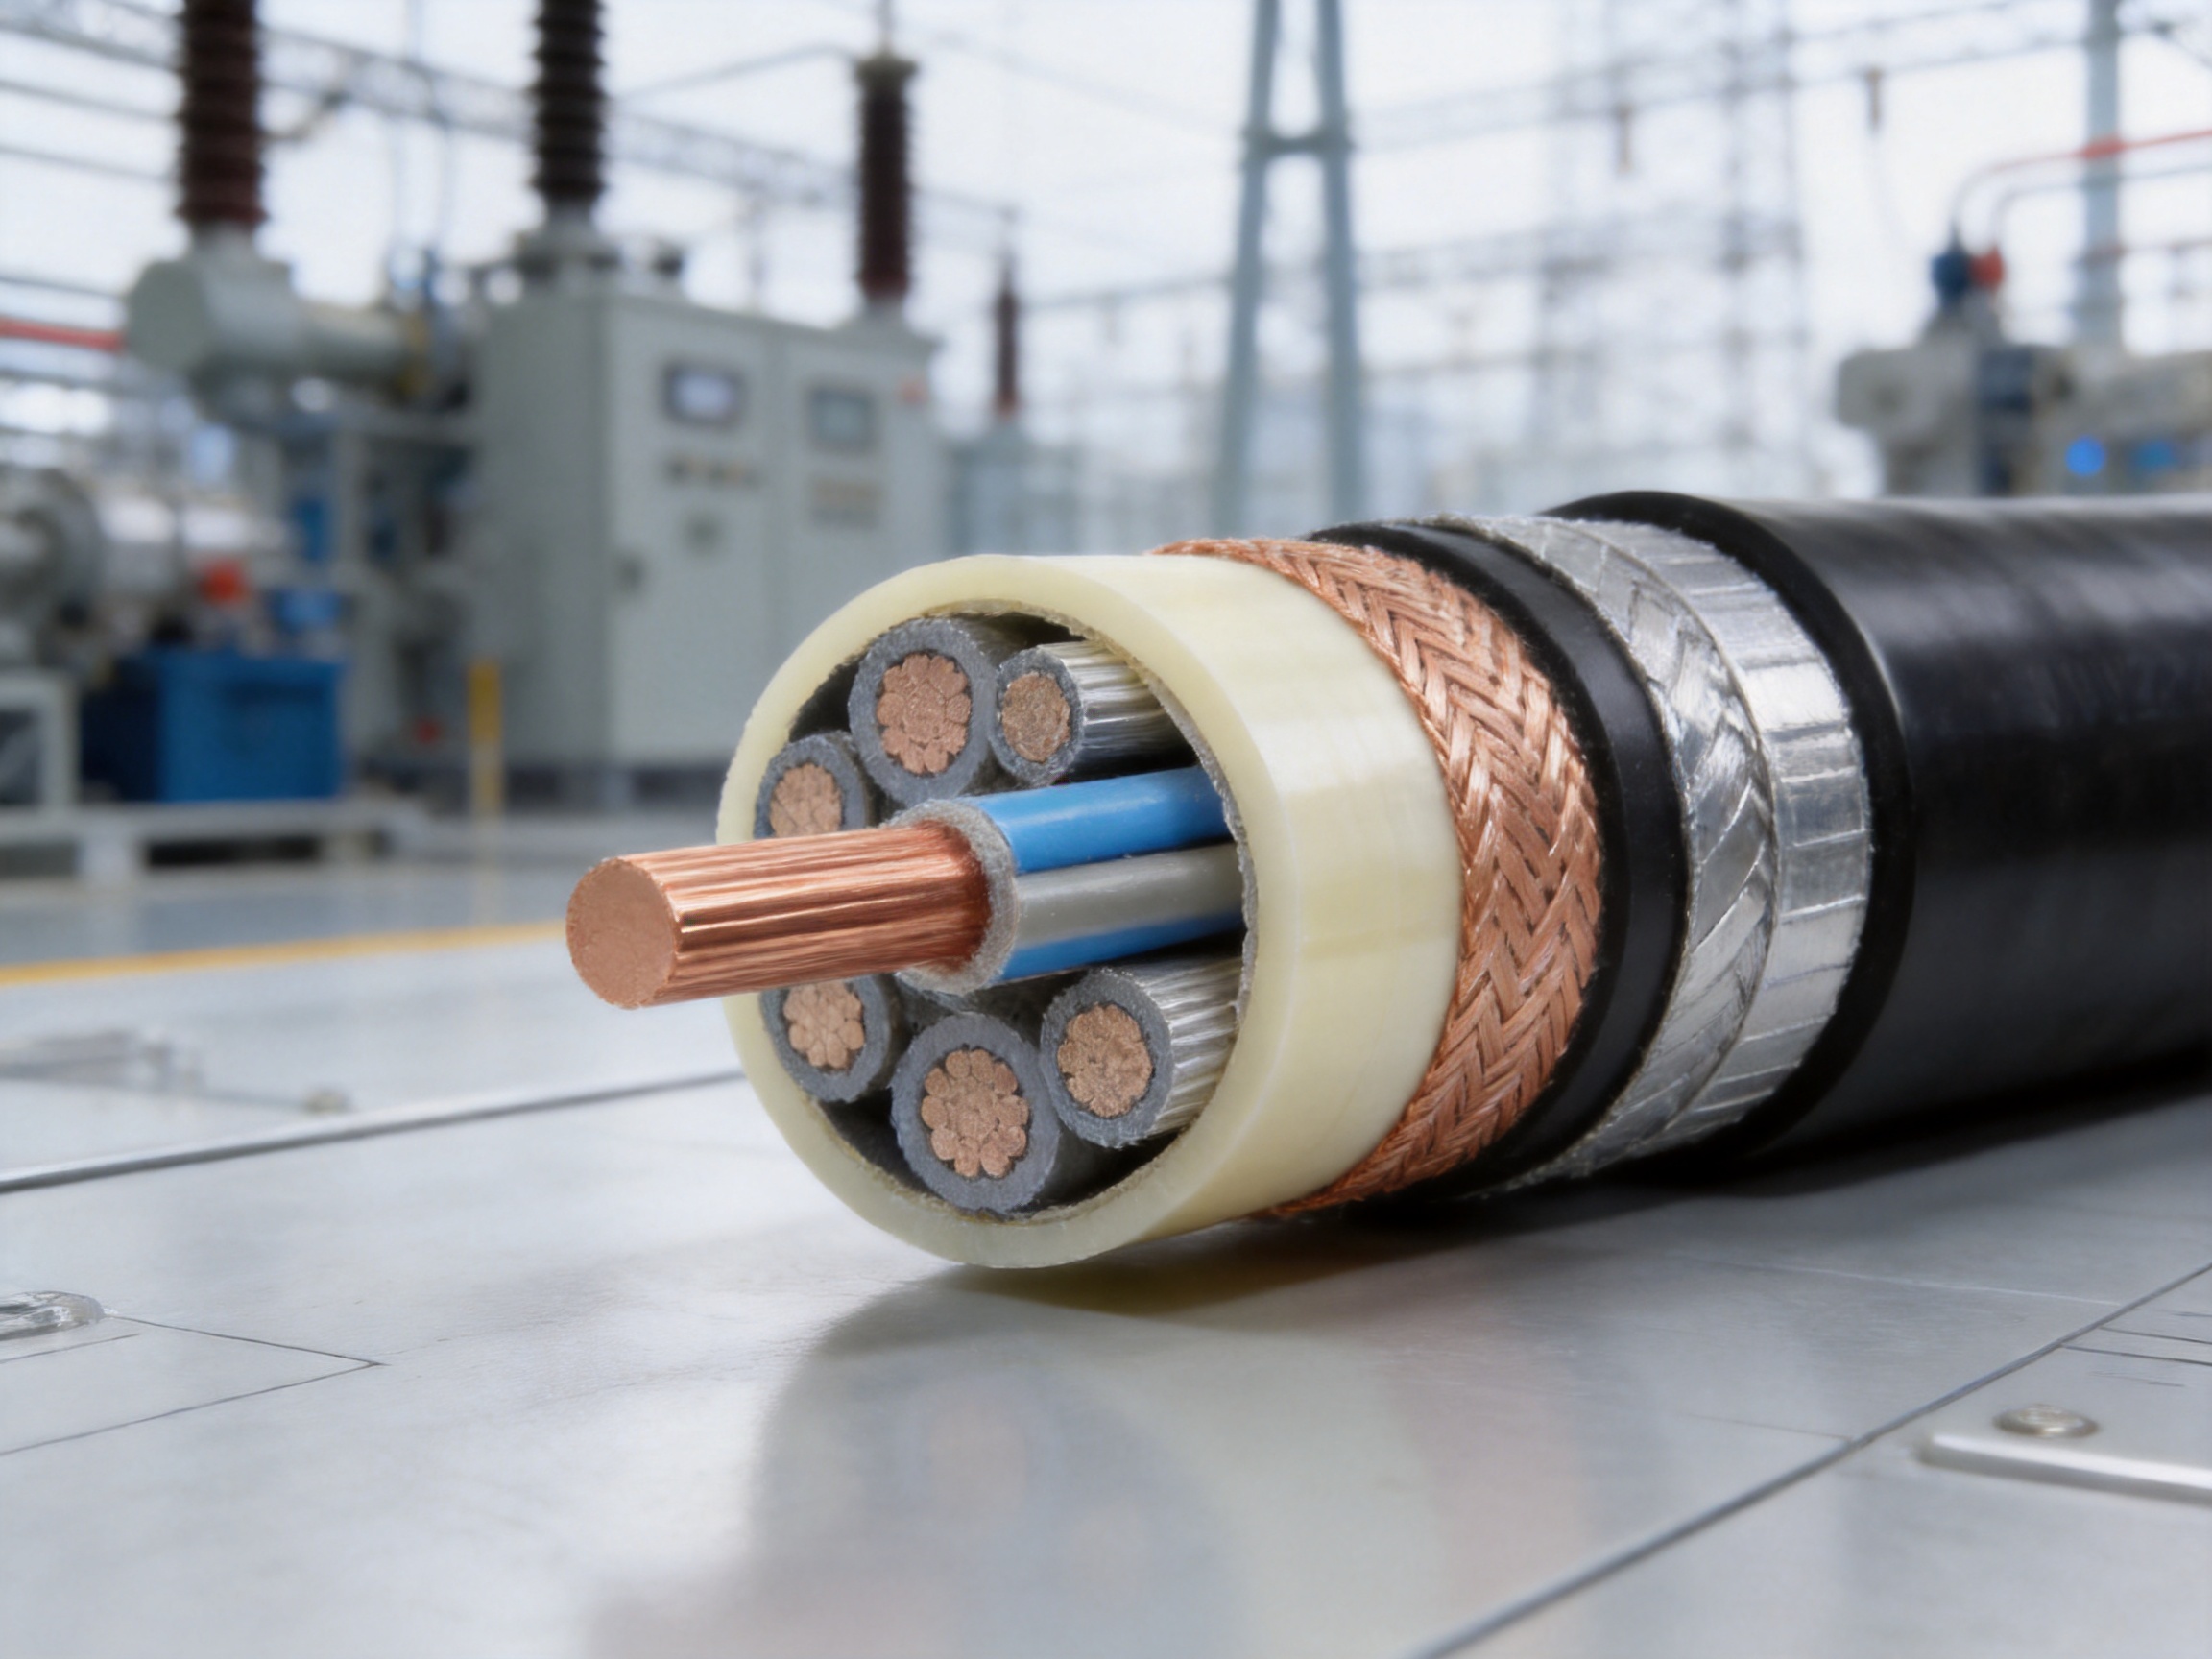
Anhui Zhishang Cable Technology Co., Ltd. integrates research and development, manufacturing, sales, and technical support. This integrated structure is valuable for products such as KYJVP22 because armored shielded cables require coordination among conductor design, insulation extrusion, shielding, armor application, sheath construction, testing, and packaging.
When technical functions are managed across one connected manufacturing organization, product adjustments can be evaluated more efficiently. Core count, conductor size, sheath material, armor arrangement, temperature requirement, flame performance, and cable identification can be discussed as parts of one complete cable design rather than as isolated purchasing items.
The company supports OEM and ODM development based on customer drawings or samples. This enables equipment manufacturers and engineering contractors to request cable constructions tailored to particular control cabinets, machinery, power projects, automation systems, or infrastructure applications.
The company operates a production base of approximately 5,000 square meters with ten automated production lines. Automation can contribute to consistent dimensional control, repeatable processing, efficient material handling, and stable production scheduling. In cable manufacturing, repeatability is important because small variations in conductor dimensions, insulation thickness, shielding coverage, armor application, or sheath concentricity can affect final performance.
Automated equipment does not replace engineering judgment or quality control. Instead, it provides a controlled platform for applying production parameters consistently. A capable production system should combine equipment control with incoming-material verification, process inspection, finished-product testing, traceability, and trained personnel.
The reported monthly production capacity of up to ten million meters supports both standard product availability and larger project requirements. Capacity is particularly important for cable projects that require multiple core counts, several conductor sizes, or coordinated delivery across different installation phases.
The company describes quality assurance based on full-core, full-length, and pure-copper specifications for standard cable models. These principles are relevant to buyers seeking predictable electrical performance and dependable delivery. Full-length attention is especially important because cable quality must remain stable throughout the manufactured drum or coil rather than only at a sampled section.
For KYJVP22, quality control should include verification of conductor material, conductor resistance, insulation integrity, insulation thickness, shield coverage, armor application, sheath dimensions, voltage performance, and visual condition. Where applicable, test reports and inspection records help customers review conformity before shipment or during incoming inspection.
The cable is specified to withstand a 3.5 kV AC test for one minute and to provide insulation resistance of at least 1000 MΩ·km at 20°C. These values support the evaluation of insulation integrity. Additional project-specific tests may be arranged when customers require particular national, international, environmental, or application-based criteria.
The organization includes quality engineers and research and development technicians with more than ten years of industry experience. Experienced technical personnel are important when a customer requires a cable that differs from a standard catalogue design.
For example, an application may require a different number of cores, a special conductor construction, a customized identification method, a flame-retardant compound, a halogen-free sheath, a particular shield termination, or a modified outer diameter. Engineering experience helps determine whether the requested features are compatible with bending radius, thermal performance, production stability, installation method, and test requirements.
Technical guidance also helps customers avoid selecting a cable solely by voltage rating. A complete selection should consider signal type, current, operating temperature, interference level, mechanical risk, environmental exposure, installation route, fire requirements, and expected service life.
Standard cable models may be stocked for faster shipment, while customized products typically require a lead time of approximately seven to twenty days, depending on construction and order details. This distinction allows customers to balance immediate availability with application-specific design.
For urgent maintenance work, stocked standard products can help reduce equipment downtime. For new industrial projects, customized production can provide better alignment with the project’s technical schedule, documentation requirements, identification system, and cable list.
Customers should confirm the production schedule before placing an order, especially when several cable types are being purchased together. The required information normally includes conductor size, core count, cable length, outer sheath color, identification marking, packaging method, test documentation, and any special fire or environmental requirements.
Production begins with the preparation of annealed copper conductors. Copper rod is processed into the required conductor form, and the conductor is checked for dimensional consistency, surface quality, and electrical continuity. Depending on the design, the conductor may remain solid or be formed into strands.
Stranding must maintain an even lay and stable diameter. Irregular stranding can affect insulation extrusion, conductor flexibility, electrical resistance, and the final cable diameter. For a multi-core cable, consistent conductor preparation helps ensure that the finished assembly remains balanced and suitable for shielding and armor application.
The prepared conductor passes through an insulation extrusion process in which XLPE is applied around the conductor. The insulation must be continuous, uniform, and free from significant voids, impurities, damage, or eccentricity.
Cross-linking changes the molecular structure of polyethylene and improves thermal stability compared with ordinary thermoplastic polyethylene. Process temperature, pressure, line speed, material quality, and cooling conditions must be controlled carefully. The objective is to obtain the required insulation thickness and dielectric performance while maintaining dimensional consistency.
After insulation, individual cores may be identified by color, numbering, or other agreed methods. Clear identification is essential for installation efficiency and helps reduce termination errors in multi-core control systems.
Insulated cores are assembled into the required cable configuration. The assembly process must maintain the intended geometry and avoid excessive stress on the individual insulated cores. Fillers or suitable assembly materials may be used when necessary to maintain roundness and support the inner sheath.
The inner PVC sheath is then applied around the core assembly. Its function is to create a stable foundation for the shield and armor while protecting the core group during subsequent manufacturing steps. The sheath thickness must remain within the design range, and the surface should be smooth and free from significant defects.
The copper braid is applied around the inner-sheathed assembly. Braid coverage, tension, angle, and continuity are important process parameters. The specified coverage of at least 80 percent provides substantial shielding while allowing the cable to retain practical installation characteristics.
Shielding equipment must maintain consistent braid formation along the cable length. Uneven tension or interrupted coverage may create weak points in electromagnetic protection. The shield should also be protected from unnecessary deformation before the armor is applied.
Galvanized steel tape is applied in two layers using a gap-wrapped arrangement. The armor must be formed with controlled overlap, spacing, tension, and alignment. Proper application helps produce consistent mechanical performance and prevents sharp edges or excessive local pressure from damaging the underlying shield or sheath.
The double-layer arrangement provides a protective barrier around the shielded core assembly. The armor process must be coordinated with the cable’s final diameter and bending requirements. Excessive armor tension can make the cable unnecessarily rigid, while insufficient control may reduce mechanical protection or create dimensional irregularities.
The final PVC outer sheath is extruded over the armored assembly. The outer sheath provides the finished cable surface and protects the armor from moisture, abrasion, and general handling exposure. Marking may be applied to identify the cable type, voltage rating, manufacturer, production information, or customer-specific requirements.
Final sheath quality depends on material formulation, extrusion temperature, line speed, cooling, and die condition. The finished surface should be inspected for scratches, bubbles, lumps, exposed armor, dimensional variation, or other defects that could affect installation and service performance.
Completed cable is inspected and tested according to the applicable product requirements and customer agreement. Tests may include conductor continuity, conductor resistance, insulation resistance, voltage withstand, dimensional inspection, shield continuity, visual inspection, and mechanical or thermal verification where required.
Cable is then wound onto drums or packaged in coils appropriate to its diameter, length, and transportation method. Proper packaging protects the cable from impact, moisture, contamination, and excessive bending during storage and delivery. Cable ends should be sealed to prevent moisture entry, and drums should be handled using suitable lifting and rolling procedures.
Power plants and substations contain transformers, switching equipment, generators, motors, protection systems, and control panels that can produce significant electromagnetic activity. Control and monitoring circuits may require shielding to reduce the risk of signal disturbance.
The armor is useful in cable trenches, equipment areas, and routes where cables may be exposed to maintenance activity or mechanical stress. The XLPE insulation supports elevated-temperature operation in areas affected by heat from electrical equipment or restricted ventilation.
Metallurgical facilities may contain furnaces, rolling equipment, casting systems, cranes, motors, and high-current busbars. These facilities can combine high ambient temperatures, mechanical hazards, dust, vibration, and electrical noise.
KYJVP22 is suitable for control and monitoring circuits in such environments when the project’s environmental and fire requirements are satisfied. Its 90°C long-term operating temperature and armored shielded construction provide a stronger design basis than an ordinary unshielded, low-temperature control cable.
Industrial automation systems depend on reliable signals from sensors, limit switches, actuators, control cabinets, and feedback devices. Electromagnetic interference from drives, motors, relays, and switching equipment may affect system stability.
The copper braid shield helps reduce interference, while the armor provides additional protection in production areas where cables are routed near machinery, walkways, or maintenance zones. Core counts from two to thirty-seven provide flexibility for individual circuits and multi-signal connections.
Cable tunnels and pipelines may expose cables to moisture, limited ventilation, restricted access, and difficult maintenance conditions. Mechanical protection is valuable because repair or replacement can be time-consuming after installation.
The cable’s inner and outer PVC sheaths help resist ordinary moisture and environmental exposure, while the armor provides a stronger barrier against mechanical damage. Tunnel projects should also evaluate fire load, smoke generation, drainage, ventilation, and emergency procedures before selecting the standard construction.
The armored construction supports selected direct-burial applications. Before using KYJVP22 underground, engineers should confirm soil conditions, burial depth, water exposure, chemical contamination, rodent risk, external loading, road crossings, jointing methods, and local code requirements.
The cable should be installed with appropriate bedding, protection, warning systems, and separation from other utilities. Sharp stones and excessive pulling tension should be avoided. The fifteen-times-outer-diameter minimum bending radius should be respected during installation, especially near cable pits, bends, and terminations.
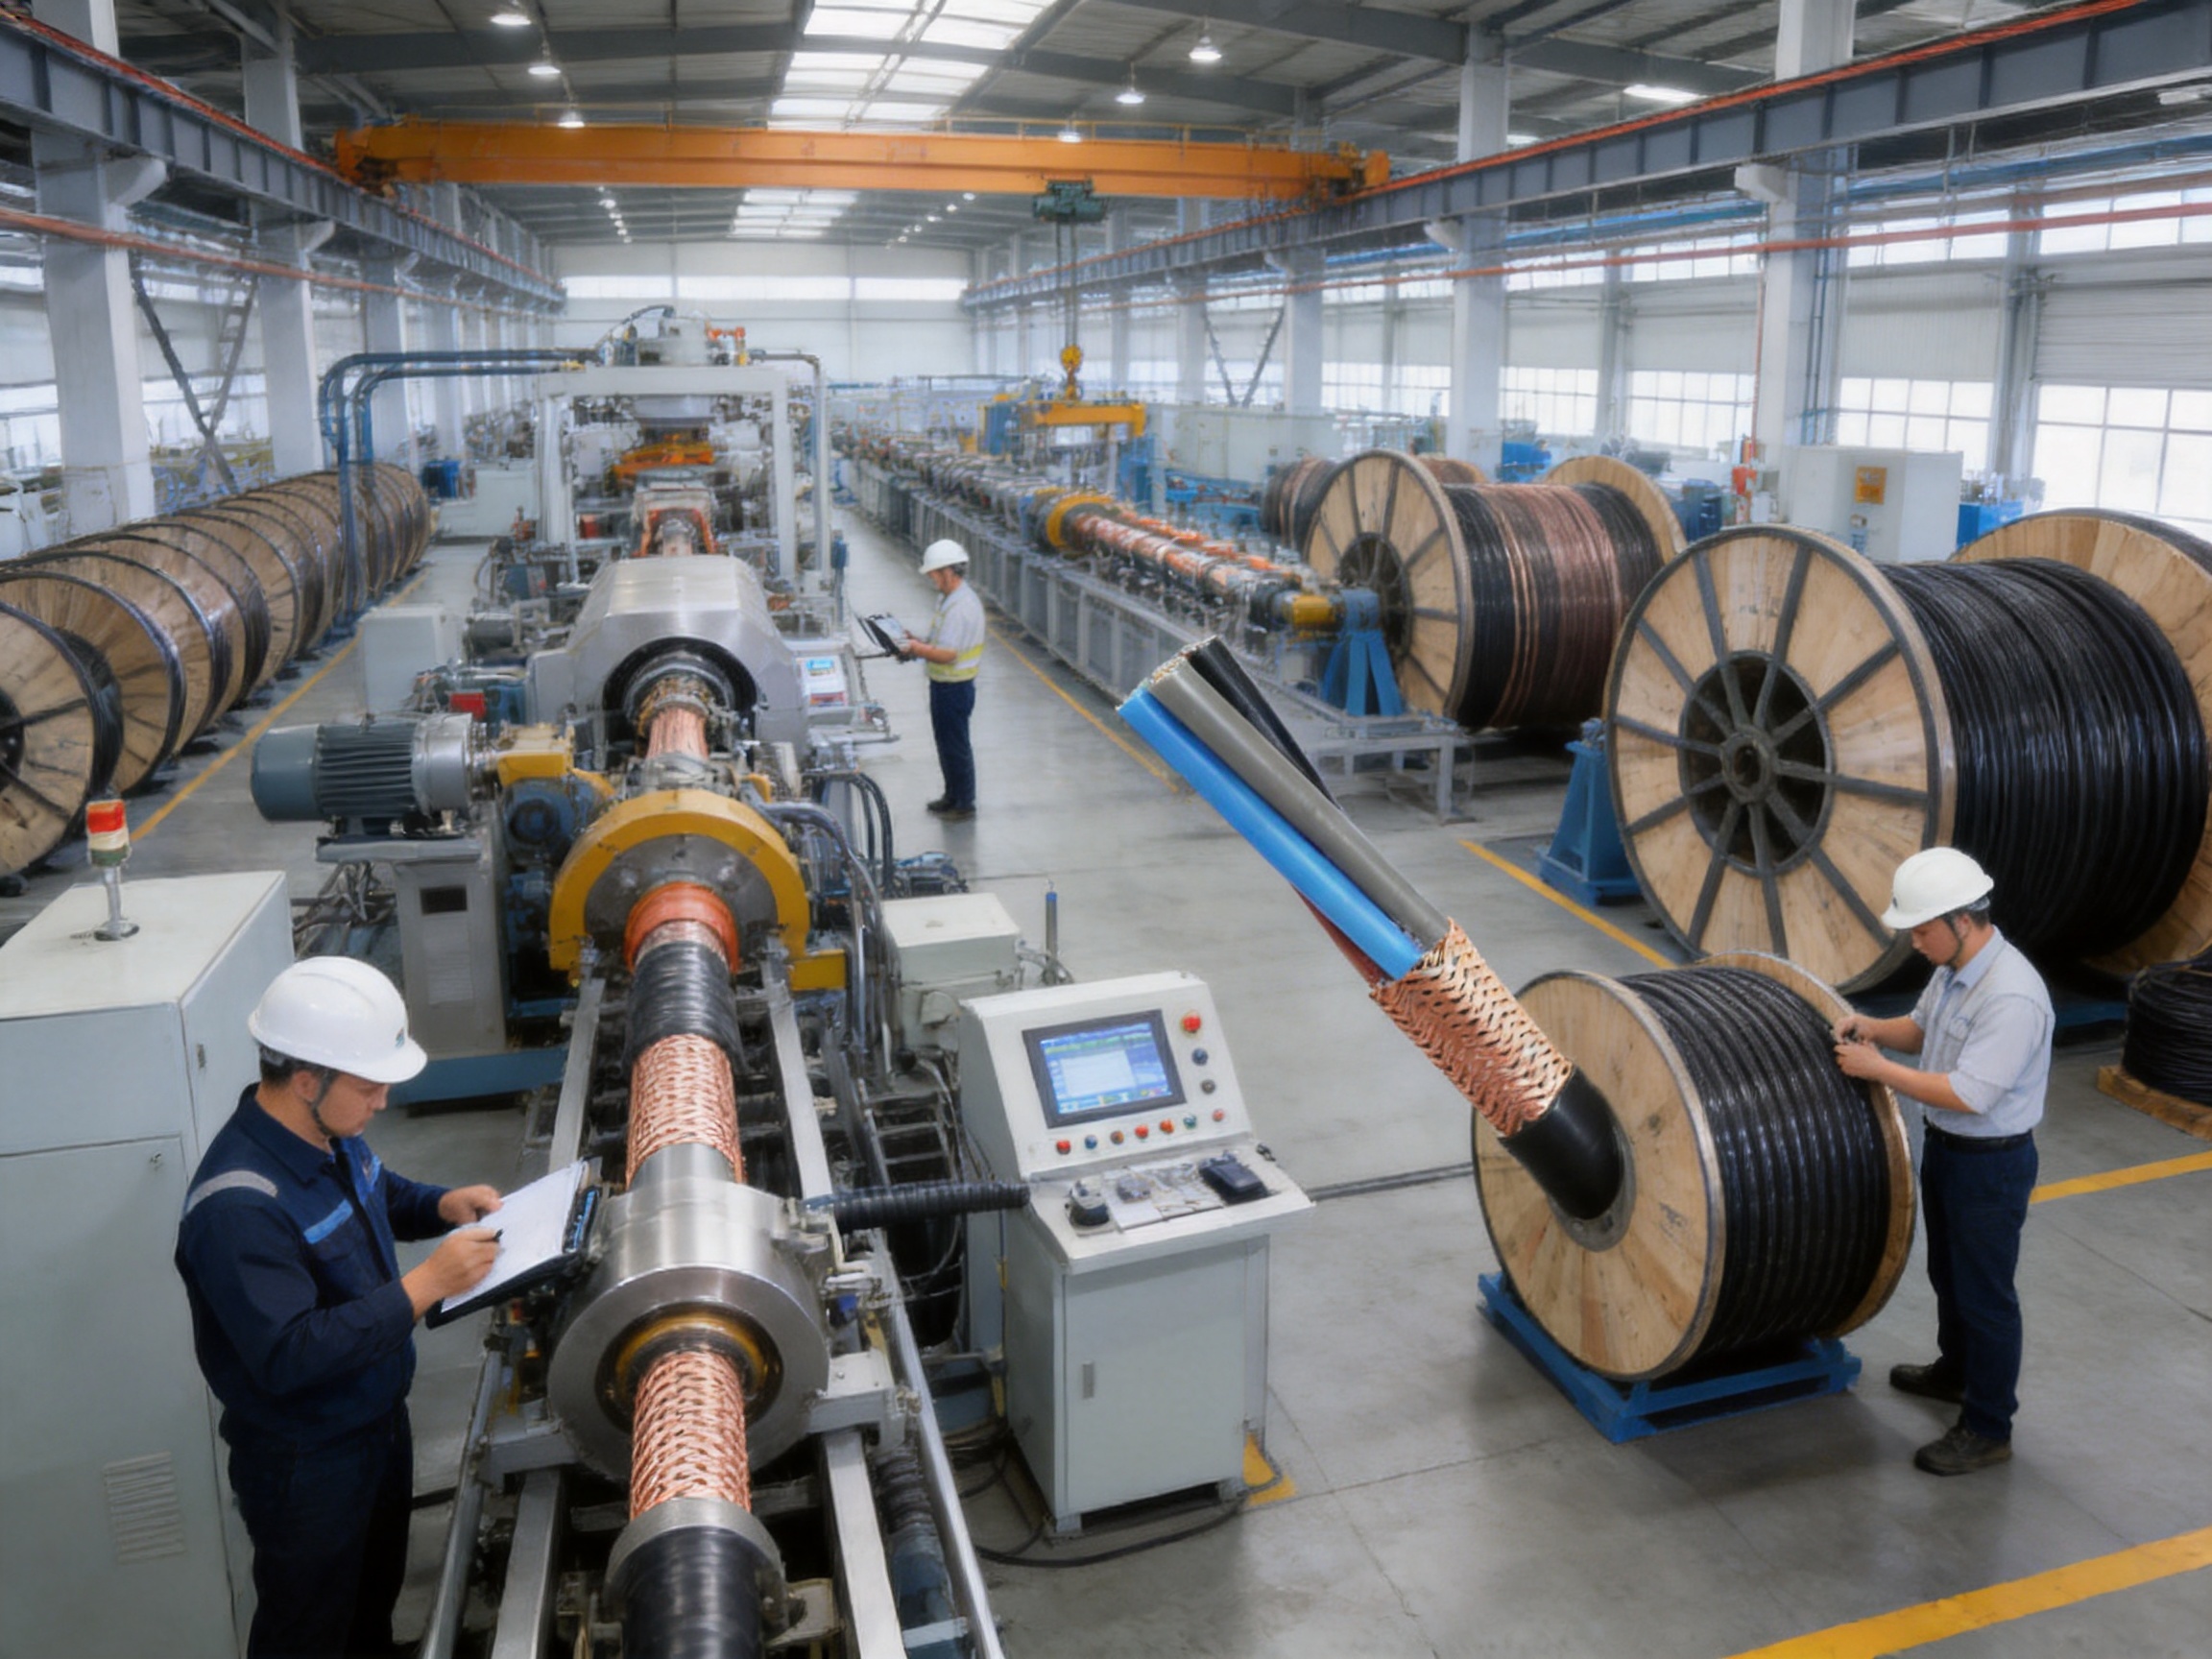
Before cable delivery, the project team should confirm the cable type, conductor size, core count, length, route, destination, termination arrangement, and identification marking. Many installation problems result from incorrect cable allocation rather than from cable material failure.
For multi-core control cables, the core numbering and termination schedule should be checked against drawings. Shield termination points should be identified in advance. If the armor is to be bonded for safety or grounding purposes, the bonding design should be coordinated with the electrical system.
Cable drums should be stored on firm, dry ground and protected against standing water, impact, and unauthorized movement. The cable ends should remain sealed. Drums should be rolled only in the indicated direction and should not be dropped or dragged.
During unwinding, the cable should be pulled from the top of the drum in a controlled manner. Excessive pulling force can damage the sheath, deform the armor, or create hidden stress in the core assembly. A suitable cable roller system is recommended for long routes and heavy armored cables.
KYJVP22 has a minimum bending radius of at least fifteen times the cable outer diameter. This requirement applies during installation and final positioning. Bending the cable too sharply may deform the armor, reduce shield continuity, damage the sheath, or place stress on the insulation.
Large-radius bends should be planned at cable entries, tray transitions, equipment connections, and underground pits. Temporary bends used during pulling should not be tighter than the permitted radius. Cable cleats and clamps should support the cable without creating local crushing forces.
The copper braid shield should remain continuous along the cable route. At terminations, the shield should be prepared carefully to avoid unnecessary braid damage. Pigtails should be kept as short as practical when the grounding design requires a low-impedance connection.
Grounding methods depend on the circuit type, frequency range, equipment design, and site grounding system. Some applications use one-end shield grounding to reduce circulating currents, while others require grounding at both ends for high-frequency interference control. The project engineer should define the method rather than applying a universal rule.
Because KYJVP22 is armored, the selected cable glands and termination accessories must accommodate the cable diameter, armor construction, sheath materials, and grounding requirements. A gland that is too small may damage the outer sheath or armor. A gland that is too large may fail to provide adequate sealing and mechanical retention.
Terminations should be completed by trained personnel using appropriate stripping tools. The XLPE insulation, copper braid, steel tape, inner sheath, and outer sheath should be exposed in a controlled sequence. The completed termination should be inspected for insulation damage, loose shield strands, exposed sharp armor edges, and inadequate sealing.
Different projects may require variations in conductor size, number of cores, identification, sheath color, cable length, packaging, and documentation. KYJVP22 is available across a relatively broad range of conductor cross-sections and core counts, and additional project-specific requirements can be discussed with the manufacturer.
Flame-retardant versions may be considered for buildings, tunnels, power facilities, and other areas where cable flame performance is important. Halogen-free options may be considered where low smoke, reduced corrosive gas emissions, or special safety requirements are specified. These alternatives should be treated as engineered variations rather than assumed properties of the standard PVC-sheathed product.
Customers can also request OEM or ODM development based on drawings or samples. A technical inquiry should include rated voltage, conductor material, cross-section, number of cores, insulation type, shielding requirements, armor requirements, sheath material, operating temperature, installation method, bending radius, fire performance, and relevant test standards.
For equipment manufacturers, customized marking can simplify assembly and maintenance. For infrastructure projects, standardized drum lengths, color coding, sequential meter marking, and project-specific documentation can improve receiving, installation, and inspection efficiency.
The first selection question is whether the installation requires all three principal functions: elevated-temperature performance, electromagnetic shielding, and mechanical protection. If the answer is yes, KYJVP22 may be more appropriate than a basic control cable.
The second question concerns the electrical circuit. Designers should verify conductor cross-section, expected current, voltage drop, fault conditions, rated voltage, and terminal compatibility. The 450/750V rating should be matched to the system voltage and applicable regulations.
The third question concerns the environment. The design team should evaluate ambient temperature, moisture, chemicals, ultraviolet exposure, vibration, impact, compression, burial conditions, fire requirements, and expected maintenance conditions.
The fourth question concerns installation. The route must accommodate the cable’s outer diameter and fifteen-times-diameter minimum bending radius. Cable trays, conduits, glands, brackets, cleats, joints, and termination boxes should all be compatible with an armored cable.
The fifth question concerns documentation and acceptance. Customers should clarify whether they require routine test reports, material declarations, inspection records, sample approval, third-party testing, or project-specific compliance documentation. Early clarification helps prevent delays after production.
Cable manufacturing requires careful control of copper, polymeric materials, steel armor, energy, packaging, and production waste. Responsible manufacturing involves efficient material usage, process stability, quality control, and reduction of rejected product.
The company emphasizes green manufacturing and responsible production practices. Consistent automated processing can support better material utilization and reduce variations that lead to rework. Longer service life also contributes to sustainability because replacement, downtime, transportation, and disposal are reduced when cable performance remains reliable.
Customers can support responsible cable use by selecting the correct conductor size, avoiding unnecessary overspecification, planning routes efficiently, protecting installed cable from avoidable damage, and disposing of removed cable through appropriate recycling channels. Copper and steel components have significant recovery value when processed through qualified recycling systems.
International buyers often need more than a product description. They require responsive engineering communication, predictable production, clear technical data, reliable packaging, and practical support during selection and installation.
Anhui Zhishang Cable Technology Co., Ltd. serves international markets including the United States, Canada, Australia, Japan, and parts of Eurasia. Its customer support model includes standard cable supply, customized development, technical selection guidance, test documentation, and warranty support for standard cable models.
For overseas projects, buyers should provide a complete technical specification at the inquiry stage. Differences among national standards, terminology, conductor classes, fire-performance classifications, environmental requirements, and inspection procedures can affect the final cable construction. A clear data exchange reduces the risk of misunderstandings and helps the manufacturer prepare an accurate quotation.
International project purchasing should also confirm packaging dimensions, drum markings, shipping conditions, delivery terms, documentation language, spare length, and storage limitations. These practical details are especially important for heavy armored cables because transportation damage or incorrect drum handling can create problems before installation begins.
KYJVP22 identifies a control cable construction that combines cross-linked polyethylene insulation, copper braid shielding, and double-layer steel tape armor, with PVC inner and outer sheaths. The exact interpretation of cable letters can vary by national designation system, so the complete technical construction should always be confirmed from the product specification.
The long-term allowable operating temperature of the conductor is 90°C. The stated fixed-installation temperature range is -15°C to +90°C. Equipment terminals, glands, surrounding materials, and installation conditions must also be suitable for the actual operating temperature.
It can be considered for control circuits in areas affected by electromagnetic interference from motors, drives, and switching equipment. The copper braid shield helps suppress interference. However, cable routing, separation, grounding, shield termination, and equipment compatibility remain essential to achieving satisfactory field performance.
The armored construction supports selected direct-burial installations. The project must evaluate soil conditions, water, chemicals, external loading, burial depth, mechanical protection, local codes, and jointing requirements. Direct burial should not be assumed suitable without a site-specific engineering review.
The supplied specification states compliance with GB/T 19666 non-flame-retardant requirements. The standard construction uses PVC inner and outer sheaths and should not automatically be treated as halogen-free. Flame-retardant and halogen-free versions may be available as customized options and must be confirmed before purchase.
The minimum bending radius is at least fifteen times the cable outer diameter. This requirement should be observed during pulling, routing, tray installation, equipment entry, and termination.
The stated range is from two cores to thirty-seven cores. The final selection depends on the control circuit schedule, conductor cross-section, cable diameter, installation space, and project requirements.
The stated cross-section range is 1.5 mm² to 10.0 mm². Solid or stranded annealed copper conductors can be considered according to the installation and termination requirements.
The shield coverage is specified as at least 80 percent, with a shielding attenuation factor of no greater than 0.8 at 1 MHz under the stated conditions. Actual performance depends on frequency, grounding, termination, cable routing, nearby interference sources, and the overall system design.
The listed specifications include a 3.5 kV AC test for one minute, insulation resistance of at least 1000 MΩ·km at 20°C, a compression strength of at least 2000 N/100 mm, an impact test associated with IEC 60229, and a 150°C four-hour thermal deformation test. Additional inspection and documentation can be discussed for specific projects.
Yes. Customization can include conductor size, core count, cable length, marking, sheath requirements, flame performance, halogen-free construction, packaging, and other technical details. OEM and ODM development can be based on customer drawings or samples.
An inquiry should identify the application, rated voltage, conductor size, number of cores, conductor type, operating temperature, installation method, electromagnetic environment, mechanical risks, fire requirements, desired length, delivery schedule, marking, packaging, and required test documentation.
No. Armor improves mechanical protection, but conduit or additional protection may still be required in areas with severe impact, special fire risks, chemical exposure, road crossings, public access, or local code requirements. The complete installation must be designed as a system.
KYJVP22 integrates thermal capability, electromagnetic shielding, and mechanical armor. A lower-cost unshielded cable may require additional separation, conduit, shielding measures, or replacement protection. The most economical choice should be based on total installed cost and reliability rather than cable purchase price alone.
KYJVP22 is a practical solution for fixed industrial control applications where ordinary cable construction may not provide enough thermal, electrical, or mechanical protection. Its XLPE insulation supports long-term operation at 90°C, its copper braid shielding helps reduce electromagnetic interference, and its double-layer galvanized steel tape armor increases resistance to compression and impact.
The product supports two to thirty-seven cores and conductor cross-sections from 1.5 mm² to 10.0 mm², making it adaptable to a broad range of control and monitoring circuits. Its PVC inner and outer sheaths provide a balanced combination of protection, processability, and cost efficiency, while customization options allow projects to consider flame-retardant, halogen-free, and other application-specific requirements.
The manufacturing capabilities of Anhui Zhishang Cable Technology Co., Ltd. strengthen the product’s value. The company combines research and development, automated production, quality engineering, technical support, OEM and ODM services, standard inventory, customized production, and international supply experience. Its production base, ten automated lines, experienced technical personnel, and reported monthly capacity of up to ten million meters support both regular orders and project-scale requirements.
For power plants, substations, metallurgical equipment, cable tunnels, automation systems, pipelines, and selected direct-burial applications, KYJVP22 offers a balanced combination of signal protection, thermal endurance, and mechanical strength. Correct cable selection, installation, grounding, termination, and environmental evaluation remain essential, but the integrated construction provides a strong technical foundation for demanding industrial systems.
1. Product technical specification for KYJVP22 armored shielded control cable, including construction, electrical characteristics, mechanical performance, and operating limits.
2. GB/T 19666, General Rules for Flame Retardant and Fire Resistant Wires and Cables.
3. IEC 60229, Electric Cables—Special Tests on Extruded Oversheaths with a Special Protective Function.
4. General principles for the design, installation, testing, and maintenance of low-voltage control and instrumentation cable systems.
5. Technical guidance on XLPE-insulated cable construction, thermal performance, insulation resistance, and voltage withstand testing.
6. Industrial cable installation practices covering cable routing, bending radius, shielding, grounding, armor bonding, termination, and drum handling.
7. Manufacturer information concerning research and development, automated production lines, OEM and ODM services, quality assurance, production capacity, and international supply support.
8. Engineering principles for electromagnetic compatibility in industrial control, automation, power-generation, and substation environments.
We firmly believe that good cables are not only a competition of materials, but also a reflection of craftsmanship, quality, and responsibility.
Links
Product
Send Inquiry
No. 29 Sankeshu Road, Xuanzhou District, Xuancheng City, Anhui Province, China
+86-18621104555/+86-563-2622999
 Electrical Cable Manufacturer
OEM/ODM Wire and Cable Solutions
 English
 Español
 عربى
 русский